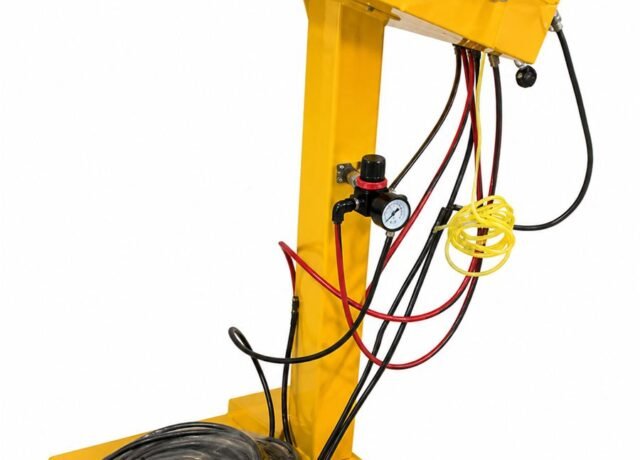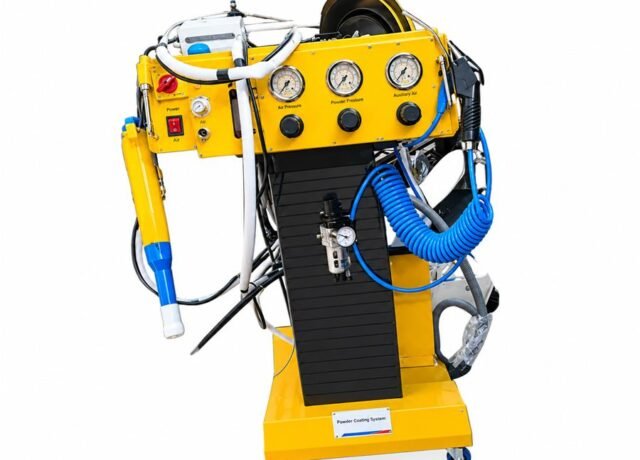
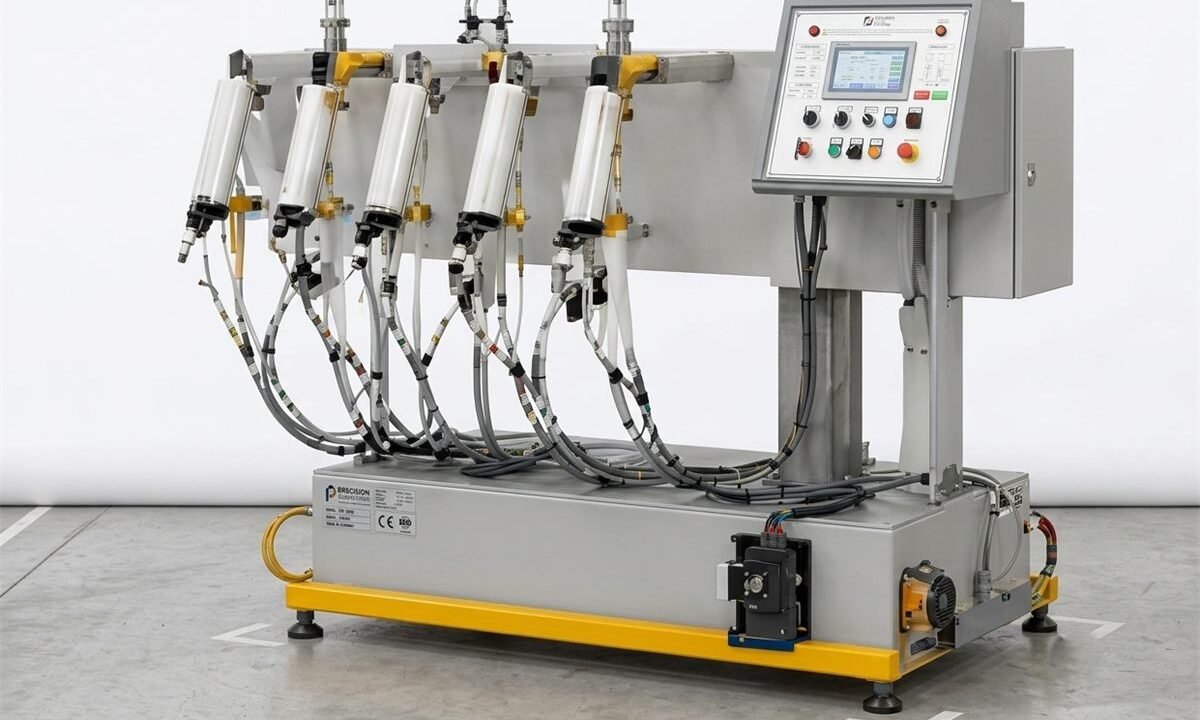
On a conveyorised line, automatic guns mounted on a vertical reciprocator sweep up and down as the components pass, giving continuous and identical coverage without an operator holding a gun in the booth all shift.
Gun count, spacing and reciprocator stroke are set from the component height and the line speed. For most jobs a bank on each side of the booth is enough; taller or more complex work takes additional guns angled to reach the areas a straight-on spray would miss.
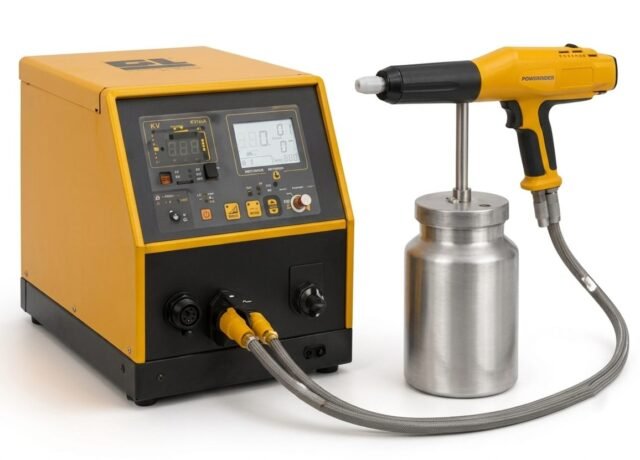
Each gun runs from its own control channel, so kV and output can be trimmed per position instead of everything moving together. Manual touch-up guns are usually kept at the booth exit for recessed areas – we supply the line so both work off the same powder feed.